English
 Español
 tiếng việt
 русский

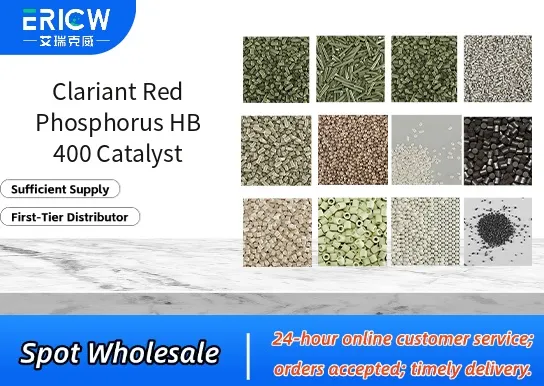
High thermal stability suitable for demanding high-temperature polymer processing conditions.
Low volatility and minimal phosphine gas emission during compounding and extrusion.
Excellent dispersion performance in engineering thermoplastics including polyamides and polyesters.
Halogen-free flame retardant catalyst enabling compliance with RoHS and REACH regulations.
Consistent batch-to-batch performance ensured through stringent Clariant quality control protocols.
Flame-retardant polyamide 6 and polyamide 66 compounds for automotive under-hood components.
Enhanced fire-safe engineering plastics used in electrical and electronic connectors.
High-performance flame-retardant polybutylene terephthalate (PBT) for industrial housings.
Thermoplastic composites requiring UL 94 V-0 rating at thin-wall sections.
| Chemical Type | Stabilized red phosphorus |
| Product Form | Free-flowing granules |
| Appearance | Dark red to burgundy granules |
| Phosphorus Content (as P) | ≥ 85.0 wt % |
| Moisture Content | < 0.3 wt % |
| Particle Size (d50) | 150–250 µm |
| Primary Applications | Halogen-free flame retardancy in polyamides, PBT, and PET |
| Key Features | Thermal stabilization, low volatility, halogen-free, RoHS-compliant |
Q1: What is the primary function of Clariant Red Phosphorus HB 400 in polymer systems?
A: Clariant Red Phosphorus HB 400 is a halogen-free flame retardant catalyst designed to promote char formation and suppress smoke generation during thermal decomposition of engineering thermoplastics—particularly polyamide (PA6, PA66) and polybutylene terephthalate (PBT).
Q2: How does HB 400 differ from conventional red phosphorus grades?
A: HB 400 features a proprietary surface treatment that enhances thermal stability, reduces hygroscopicity, and improves compatibility with polar engineering resins—resulting in better dispersion, reduced corrosion potential, and improved long-term color stability compared to untreated or minimally stabilized red phosphorus.
Q3: Is HB 400 suitable for applications requiring regulatory compliance for food contact or electronics?
A: HB 400 is formulated for high-purity performance and has been evaluated in systems targeting UL 94 V-0 and glow-wire ignition temperature (GWIT) compliance. While it is not inherently certified for food contact or RoHS-exempted electronics use, its low volatility and controlled phosphorus release profile support qualification efforts in regulated end-use segments—subject to full system validation.
Q4: What processing considerations should be taken when compounding with HB 400?
A: Due to its reactivity at elevated temperatures, HB 400 should be introduced downstream in twin-screw extrusion or added during final melt mixing under inert atmosphere where feasible. Avoid prolonged residence time above 280 °C in oxygen-rich environments to maintain optimal performance and minimize discoloration.
Q5: How is HB 400 typically dosed in flame-retardant formulations?
A: Dosage depends on formulation requirements and target flame performance, but HB 400 is generally used at low concentrations—typically ranging from 0.1% to 2% by weight—in combination with synergists such as melamine polyphosphate or metal phosphinates to achieve balanced flame retardancy, mechanical retention, and processability.
Contact With Us:
E-mail: wangxingqiang@ericwchem.com
Have a Questions? Call Us:
Add:
Building A1, Jiete Industrial Park, Huangpu District, Guangzhou City, Guangdong Province, China